FILAMENT NONWOVEN GEOTEXTILE
Filament Spunbond Needle-Punched Nonwoven Geotextile
A PET- or PP-filament nonwoven geotextile produced through melt spinning, air-laid web formation and needle-punch consolidation for reinforcement, filtration, separation and drainage in civil and environmental engineering applications.
PRODUCT OVERVIEW
Filament Geotextile for Reinforcement, Filtration, Separation and Drainage
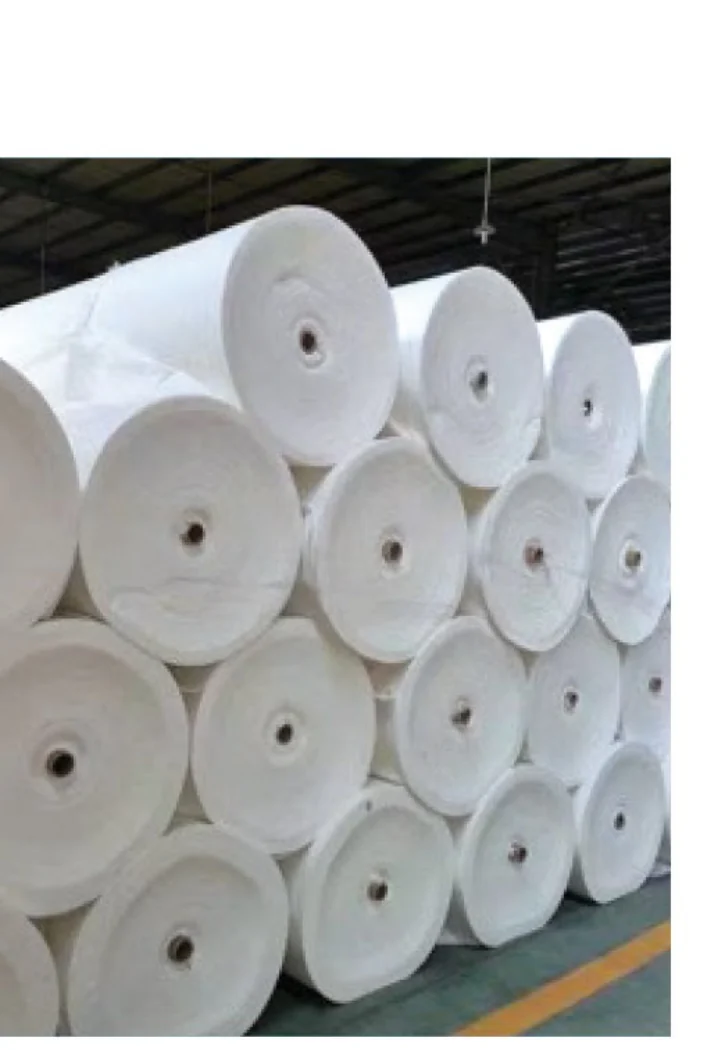
The listed raw-material basis is PET or PP. The nonwoven material is formed through melt spinning, air-laid web formation and needle-punch consolidation.
Reference standards listed for the product are GB/T 17639-2008 and JT/T 519-2004. Material, performance class, roll width and acceptance requirements should be confirmed for the specific project and order.
MATERIAL & NONWOVEN STRUCTURE
Filament Material Formed into a Three-Dimensional Porous Structure
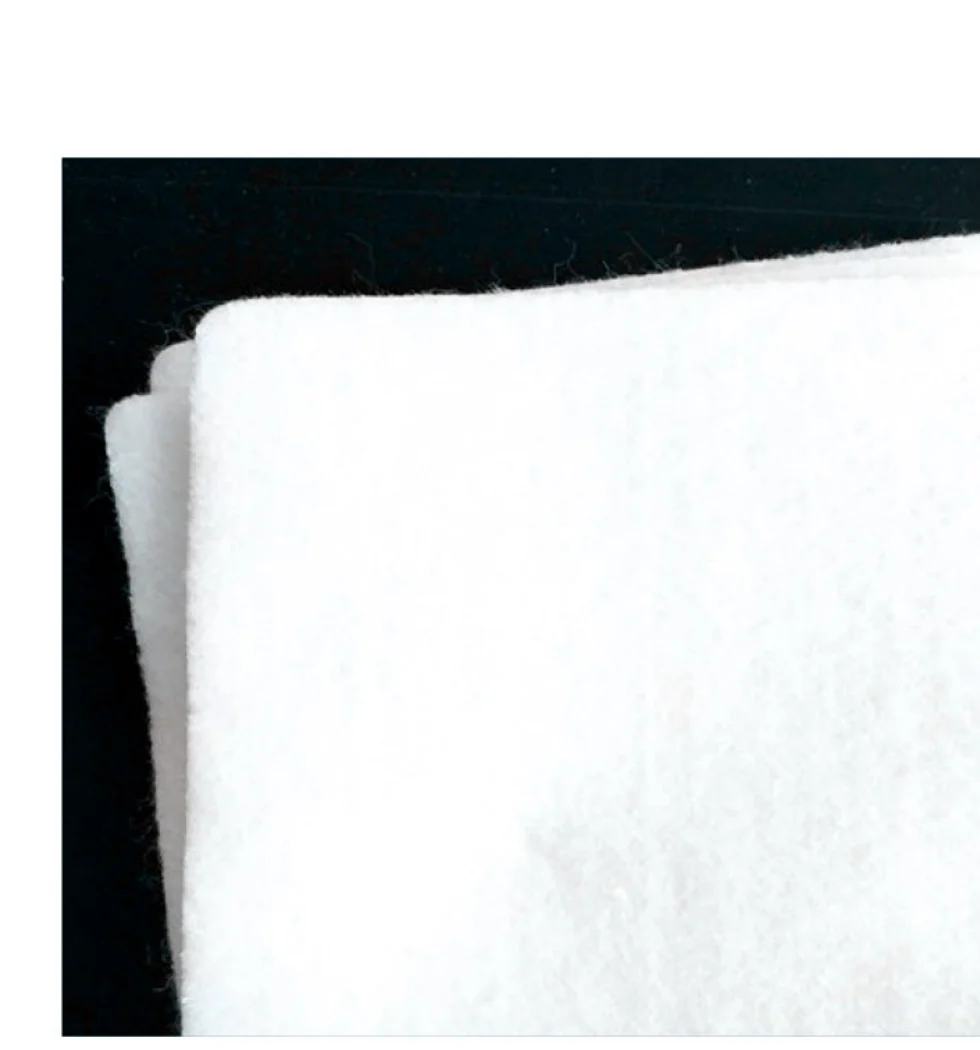
Produced from PET or PP through melt spinning, air-laid web formation and needle-punch consolidation, forming a nonwoven geotextile with a three-dimensional porous structure.
PET or PP
The required polymer basis should be identified in the project or procurement specification.
Melt spinning
The filament material is produced through a melt-spinning process.
Air-laid web formation
The filaments are formed into a nonwoven web before consolidation.
Needle-punch consolidation
Needle punching consolidates the web into a three-dimensional porous geotextile structure.
APPLICATIONS
Engineering Contexts for Filament Geotextile Selection
Application conditions, required function and project specifications should be considered together when defining the geotextile requirement.
Water Conservancy & Hydropower
Reinforcement, filtration, separation and drainage requirements may govern product selection.
Environmental Engineering
Material and performance requirements should be aligned with the environmental project specification.
Highways & Railways
Mechanical and hydraulic criteria should be reviewed against the required engineering function.
Dams & Coastal Engineering
Site conditions, filtration requirements and separation functions should be defined before procurement.
Metallurgical & Mining Applications
Product selection should follow the project specification and applicable acceptance requirements.
TECHNICAL PARAMETERS
Filament Geotextile Performance Parameters
The performance-class table below follows the listed GB/T reference. JT/T 519-2004 is also identified as a reference standard; no separate JT/T parameter table is added.
A. Availability & Dimensions
The listed product range defines areal mass and roll width. Thickness requirements are presented only within the performance-class table.
- Areal mass
- 100–1000 g/m²
- Width
- 4–7 m
B. GB/T 17639-2008 Performance Classes
Nominal breaking-strength classes and corresponding mechanical and minimum-thickness requirements.
| Property / Item | 4.5 kN/m | 7.5 kN/m | 10 kN/m | 15 kN/m | 20 kN/m | 25 kN/m | 30 kN/m | 40 kN/m | 50 kN/m |
|---|---|---|---|---|---|---|---|---|---|
| Longitudinal / transverse breaking strength kN/m | ≥4.5 | ≥7.5 | ≥10.0 | ≥15 | ≥20.0 | ≥25 | ≥30.0 | ≥40.0 | ≥50.0 |
| CBR bursting strength kN | ≥0.8 | ≥1.6 | ≥1.9 | ≥2.9 | ≥3.9 | ≥5.3 | ≥6.4 | ≥7.9 | ≥8.5 |
| Longitudinal / transverse tearing strength kN | ≥0.14 | ≥0.21 | ≥0.28 | ≥0.42 | ≥0.56 | ≥0.70 | ≥0.82 | ≥1.10 | ≥1.25 |
| Minimum thickness mm | ≥0.8 | ≥1.2 | ≥1.6 | ≥2.2 | ≥2.8 | ≥3.4 | ≥4.2 | ≥5.5 | ≥6.8 |
On smaller screens, scroll horizontally within the table. The first Property / Item column remains visible while the performance classes move horizontally.
C. Common Performance Indicators
Common requirements listed across the performance classes.
| Property / Item | Listed requirement |
|---|---|
| Elongation corresponding to nominal breaking strength % | 40–80% |
| Equivalent opening size O90(O95) mm | 0.05–0.20 mm |
| Vertical permeability coefficient cm/s | K × (10−1–10−3) cm/s, K = 1.0–9.9 |
| Width deviation % | −0.5% |
Final product configuration and acceptance requirements should be confirmed against the project specification and contract.
SELECTION CONSIDERATIONS
Information to Define Before Product Selection and Procurement
A clear inquiry should identify the functional, dimensional and performance requirements that govern product review and acceptance.
Application
State the required reinforcement, filtration, separation or drainage function and relevant site conditions.
Raw material requirement
Identify whether the project specification requires PET or PP.
Areal mass
Provide the stated areal mass and any applicable acceptance requirement.
Strength class
Identify the nominal longitudinal and transverse breaking-strength class.
Roll width
Confirm the required roll width for procurement and site handling planning.
CBR bursting & tearing
Define the mechanical requirements associated with the selected performance class.
Class-associated thickness
Review the minimum thickness requirement associated with the selected class.
Equivalent opening size
Confirm the required opening-size criterion for the intended filtration function.
Vertical permeability
State the permeability requirement governing filtration or drainage review.
Project specification
Provide the governing specification, documentation needs and contractual acceptance requirements.
MANUFACTURING & QUALITY
Align Manufacturing and Quality Review with the Confirmed Requirement
The listed manufacturing route combines melt spinning, air-laid web formation and needle-punch consolidation. Procurement review should align material, dimensional and performance requirements with the required inspection and documentation package.
- PET or PP material requirement
- Stated areal mass and roll width
- Applicable performance class and common indicators
- Thickness, opening-size, permeability and mechanical review requirements
- Required inspection records and procurement documents
TECHNICAL DOCUMENTATION
Coordinate Technical Information with the Project Specification
Product information and procurement documentation should be discussed against the confirmed material, performance class and project requirements.
Request Product and Project-Specific Information
Share the material basis, areal mass, strength class, width, mechanical and hydraulic requirements, project specification and documentation needs.
FAQ
Filament Nonwoven Geotextile Questions
Concise product and procurement information for initial specification review.
What raw materials are listed for the filament geotextile?
PET or PP is listed as the raw-material basis. The required polymer should be confirmed for the specific project and order.
What are the available areal mass and width ranges?
The stated areal-mass range is 100–1000 g/m², and the listed width range is 4–7 m.
How is the filament nonwoven structure produced?
The listed manufacturing route uses melt spinning, air-laid web formation and needle-punch consolidation to form a three-dimensional porous structure.
Which reference standards are listed?
GB/T 17639-2008 and JT/T 519-2004 are listed. The performance-class table on this page is presented under the GB/T reference; no separate JT/T data table is added.
What performance classes are shown?
The listed nominal breaking-strength classes are 4.5, 7.5, 10, 15, 20, 25, 30, 40 and 50 kN/m.
What information is needed for product selection?
Provide the application, required polymer, areal mass, strength class, roll width, bursting, tearing and class-associated thickness requirements, opening size, vertical permeability, project specification and acceptance requirements.
PROJECT & PROCUREMENT SUPPORT
Discuss Your Filament Geotextile Requirements
Share the application, material requirement, areal mass, strength class, roll width, mechanical and hydraulic requirements, project specification and documentation needs with our team.